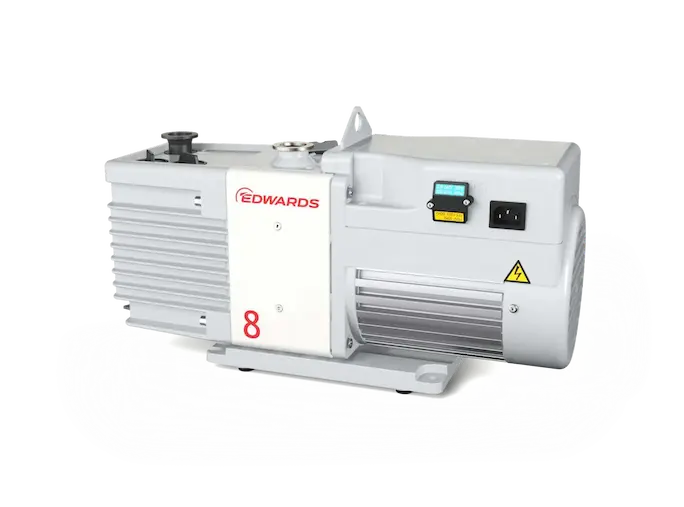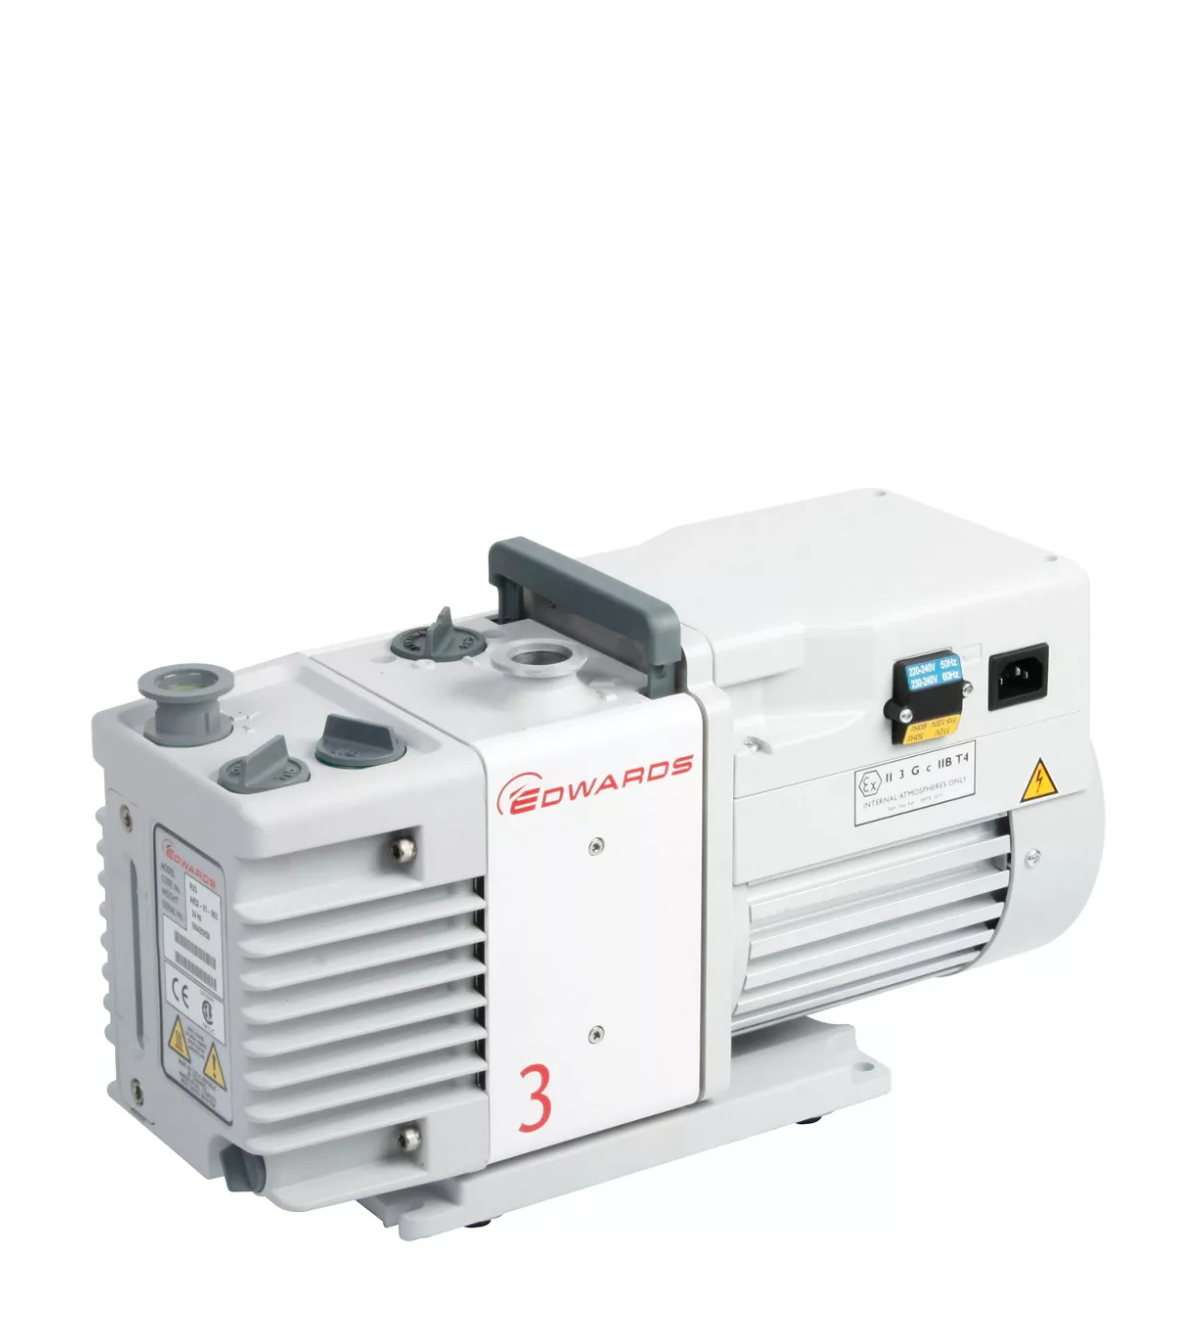
EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

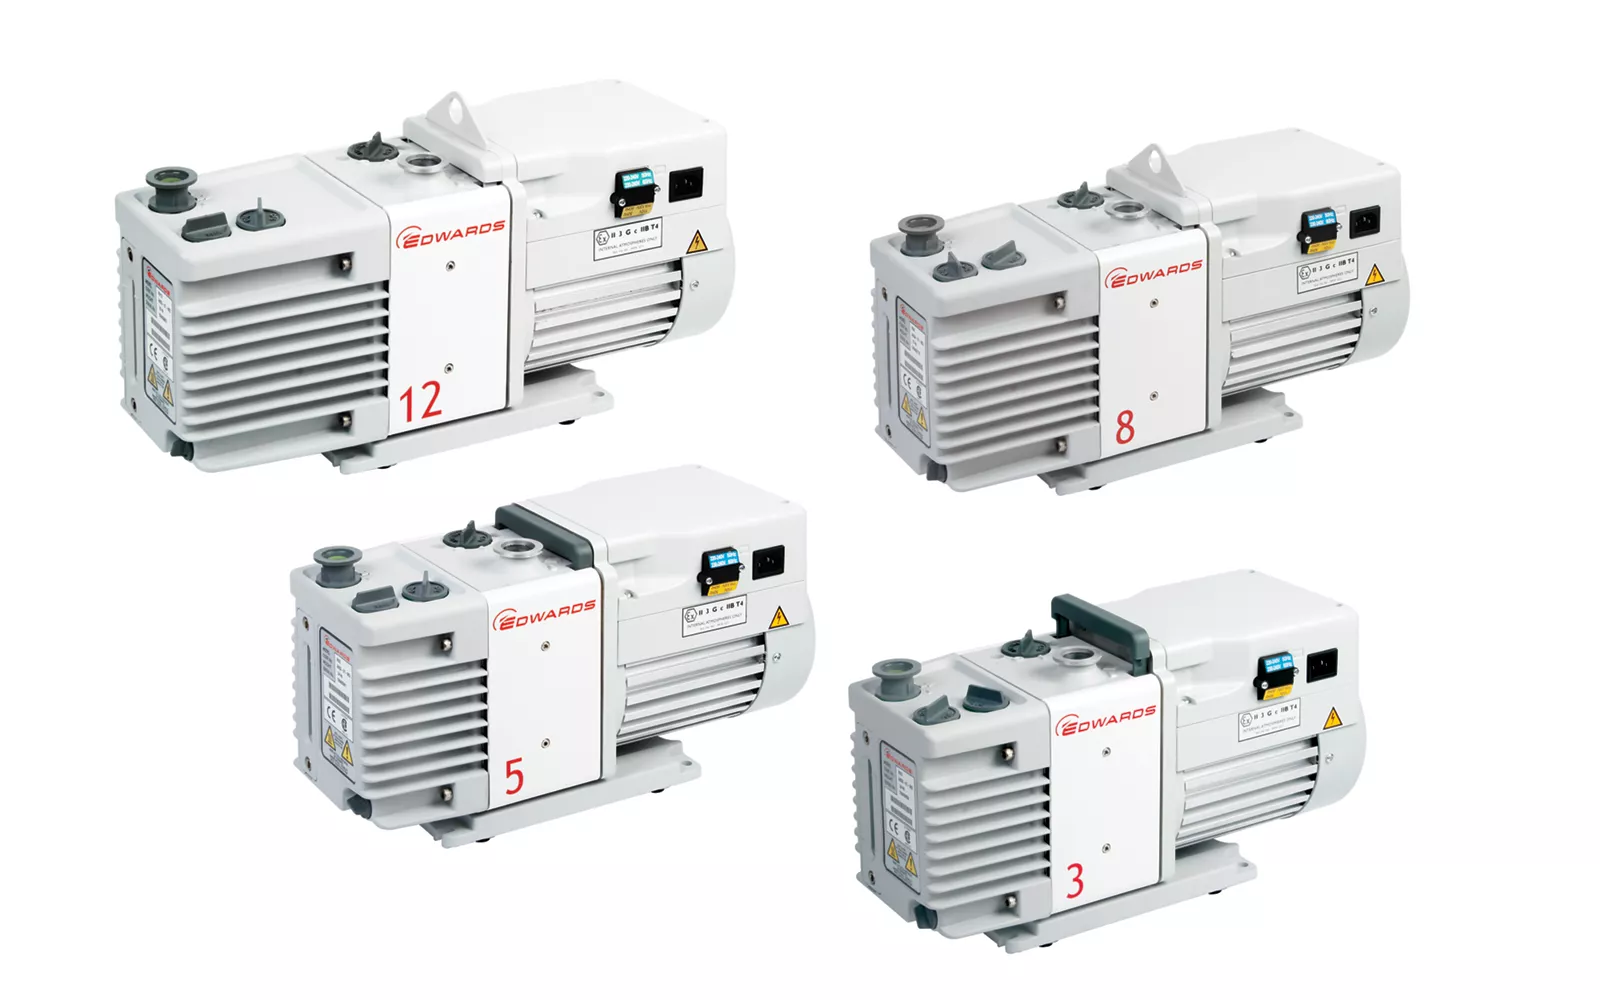
RV3 │ RV5 │ RV8 │ RV12

EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

https://drive.google.com/file/d/1-Eby8rlL7SMYYNEgl4tIm3ACLM4eqC7W/view?usp=sharing

EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

The EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps are a compact range designed for applications requiring high vacuum, stable performance, and a high capacity for vapor handling. The RV series is the industry standard for small oil-sealed rotary vane pumps.

With peak pumping speeds ranging from 3.3 to 12 m³/h at 50 Hz and an ultimate total pressure down to 2 × 10⁻³ mbar, the RV3, RV5, RV8, and RV12 models cover a wide range of scientific, analytical, laboratory, and industrial process applications.

The range is particularly notable for its mode selector, which allows the pump's operation to be adapted for high-throughput or high-vacuum applications, and its two-position gas ballast, designed to improve vapor handling.

Contact us
Variants EDWARDS RV Two-Stage Oil-Sealed Rotary Vane Vacuum Pumps – Key Features
Ultragrade Standard version lubricated with ULTRAGRADE™ Performance 19 mineral oil
PFPE PFPE-prepared pump for oxygen-rich applications; Fomblin® fluid must be ordered separately
Single-Phase Several voltage configurations available: 100/200 V or 115/230 V, depending on the model
Three-Phase IE2 Three-phase versions available depending on model and voltage
ATEX Pumps equipped with ATEX-certified explosion-proof motors available for special applications

Availability:

In stock or 8 to 10 weeks

Key performance features of EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

(indicative data, adaptable according to configuration)
Technical Characteristics EDWARDS RV Two-Stage Oil-Sealed Rotary Vane Vacuum Pumps
Maximum pumping speed 3.3 to 12 m³/h at 50 Hz
3.9 to 14.2 m³/h at 60 Hz
Ultimate pressure 2 × 10⁻³ mbar
Lubrication Positive-pressure oil lubrication
Inlet connection DN 25
Outlet connection DN 25
Single-phase motor power 0.45 to 0.55 kW
Three-phase motor power 0.25 to 0.55 kW
Weight 25 to 29 kg
Power supply 50/60 Hz single-phase or three-phase motor, depending on version
Noise level at 50 Hz 48 dB(A) and 41 dB(A) with acoustic enclosure
Operating temperature 12 to 40 °C
Maximum water vapour handling capacity Up to 290 g/h with GB II on RV12

Key benefits for your processes with EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

  • High and stable vacuum, with an ultimate total pressure reaching 2 × 10⁻³ mbar.
  • Integrated mode selector, allowing the pump to be adapted for high-throughput or high-vacuum requirements.
  • Efficient vapor handling, thanks to the two-position gas ballast.
  • Protection against oil suck-back, thanks to an automatic fast-acting inlet valve.
  • Quiet operation, with a noise level of 48 dB(A) at 50 Hz.
  • Positive-pressure oil lubrication, helping ensure reliable lubrication of the pumping mechanism.
  • Easy maintenance, thanks to a design that allows for disassembly with simple tools and simplified access to components.
  • Ultragrade or PFPE-prepared configurations, allowing the pump to be adapted to process constraints.
  • Compact footprint, particularly well-suited for scientific, analytical, and laboratory equipment.

Typical applications for EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

  • Mass spectrometry and analytical instruments. The RV range is suitable for mass spectrometry and analyticalequipment, including GCMS, LCMS, ICPMS, MALDI-TOF, and RGA, as well as surface science instruments and leak detection systems.
  • High-energy physics and accelerators. RV pumps can be integrated into beamlines, accelerators, mobile pumping carts, and laser evacuation systems. They can also provide backing for turbomolecular pumps.
  • Laboratories and sample preparation. RV pumps meet the needs of freeze dryers, rotary evaporators, concentrators, as well as distillation, extraction, and filtration operations.
  • Gel dryers and industrial processes for various industrial applications such as freeze drying, degassing, oil or epoxy resin curing, gas cylinder filling and emptying, or the manufacturing of refrigeration systems.
  • Research and development. RV pumps are also intended for R&D facilities, particularly for chamber evacuation, deposition systems, and backing turbomolecular pumps.
EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

Why choose GEFI for your EDWARDS RV two-stage oil-sealed rotary vane vacuum pumps

At GEFI, we apply our industrial vacuum expertise to help you select the EDWARDS RV oil-sealed rotary vane vacuum pump best suited to your application and operating conditions.

Technical expertise in vacuum technologies and their applications. Personalized support to select the RV3, RV5, RV8, or RV12 model suited to your required pumping speed.

Advice on vacuum levels and vapor handling based on process constraints. Support in selecting the appropriate pump and motor configuration, including Ultragrade, PFPE-prepared, single-phase and three-phase versions.

Advice on accessories, including inlet traps, oil mist filters, oil return kits, and vibration isolators. A single point of contact, from defining your needs to supplying your equipment.

Need an EDWARDS RV two-stage oil-sealed rotary vane vacuum pump or technical advice? Contact the GEFI team to select the model and configuration suited to your application

Ask for your custom study

Our experts support you in choosing, integrating and optimizing your industrial vacuum solution.

Ready to empty your mind with us?

Our team supports you in all your Industrial Vacuum and pressure projects.